The Importance of Food Safety in Plant-Based Production

The Importance of Food Safety in Plant-Based Production

  • Food safety must be integrated from the design stage of the plant-based product, not only checked at the end: raw materials, process, packaging, storage, and traceability must be defined from the outset.
  • Controls depend on each product and process: microbiology, metals, moisture, temperature, heat treatment, shelf life, allergens, and finished product must be validated according to risk.
  • Industrial validation and traceability are key to scale-up: they enable safe, repeatable, and controlled manufacturing, reducing incidents, waste, and supply risks.

Food safety in plant-based production is a fundamental aspect of ensuring that a product is safe, stable and suitable for commercialisation. In an industry that involves a wide variety of raw materials, formulations, manufacturing processes and product formats, each development requires specific controls tailored to its characteristics.

For manufacturers, food safety does not end when the product leaves the production line. It covers everything from the receipt and control of raw materials through to manufacturing, packaging, storage and the traceability of every batch. Together, these measures help reduce risks, maintain product stability and ensure a reliable supply chain.

Why Is Food Safety Critical in Plant-Based Production?

Plant-based products can involve very different raw materials and manufacturing processes, each with specific control requirements. For this reason, food safety should be considered from the product design stage and subsequently adapted to real manufacturing conditions.

Specific Risks in Plant-Based Ingredients and Products

Raw materials used in plant-based products can present different microbiological, physical and physicochemical characteristics. In addition, depending on the product, manufacturing may involve processes such as extrusion, thermal treatment, frying or chilled storage.

This means that the required controls are not exactly the same for every product. For example, in a plant-based texturate produced using dry extrusion, moisture levels may need to be controlled to ensure the product reaches the required level of dehydration. In products that undergo thermal processing, it is essential to verify that the target temperatures are achieved during manufacturing.

For this reason, food safety should be managed specifically for each product and process, with appropriate control measures established for every application.

Impact on Quality, Shelf Life and Supply Continuity

Food safety is closely linked to product stability and shelf life. Controls carried out during manufacturing and on finished products help verify that products meet defined requirements and maintain their characteristics throughout their intended shelf life.

A well-established control system also helps prevent incidents that could affect production, generate waste or compromise supply continuity. For products developed for third parties, consistency is particularly important. The product must be manufactured repeatedly while maintaining its specifications from batch to batch.

Critical Food Safety Control Points in Plant-Based Manufacturing

Food safety controls are defined according to the characteristics of each product and its manufacturing process. Common measures include microbiological testing, metal detection, in-process controls and finished product analysis.

Receipt and Control of Raw Materials

Food safety begins before raw materials enter production. Their receipt and inspection help confirm that they comply with established requirements and are suitable for manufacturing.

Supplier approval and evaluation also play a key role. Working with suppliers that meet predefined standards helps maintain consistent control over raw materials and reduces risks across the supply chain.

Processing, Mixing and Thermal Treatment

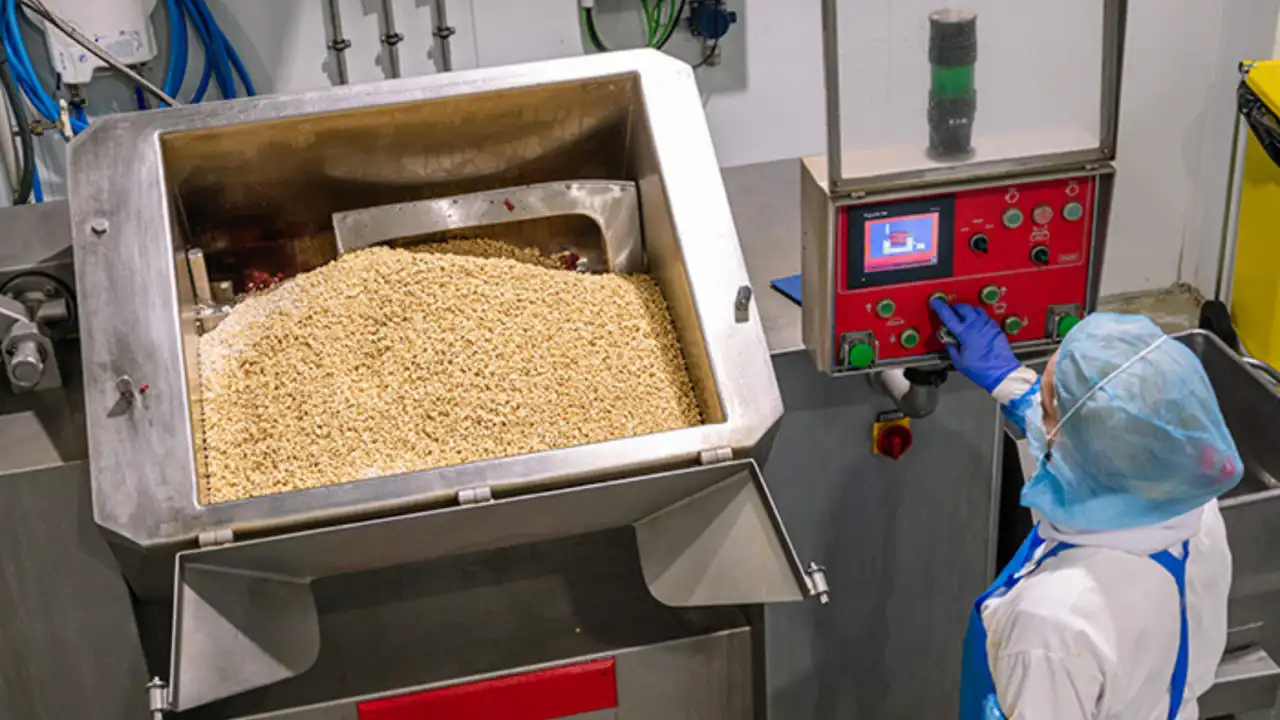
During manufacturing, controls tailored to each process are implemented. These may include parameters such as temperature, moisture and other variables relevant to the product.

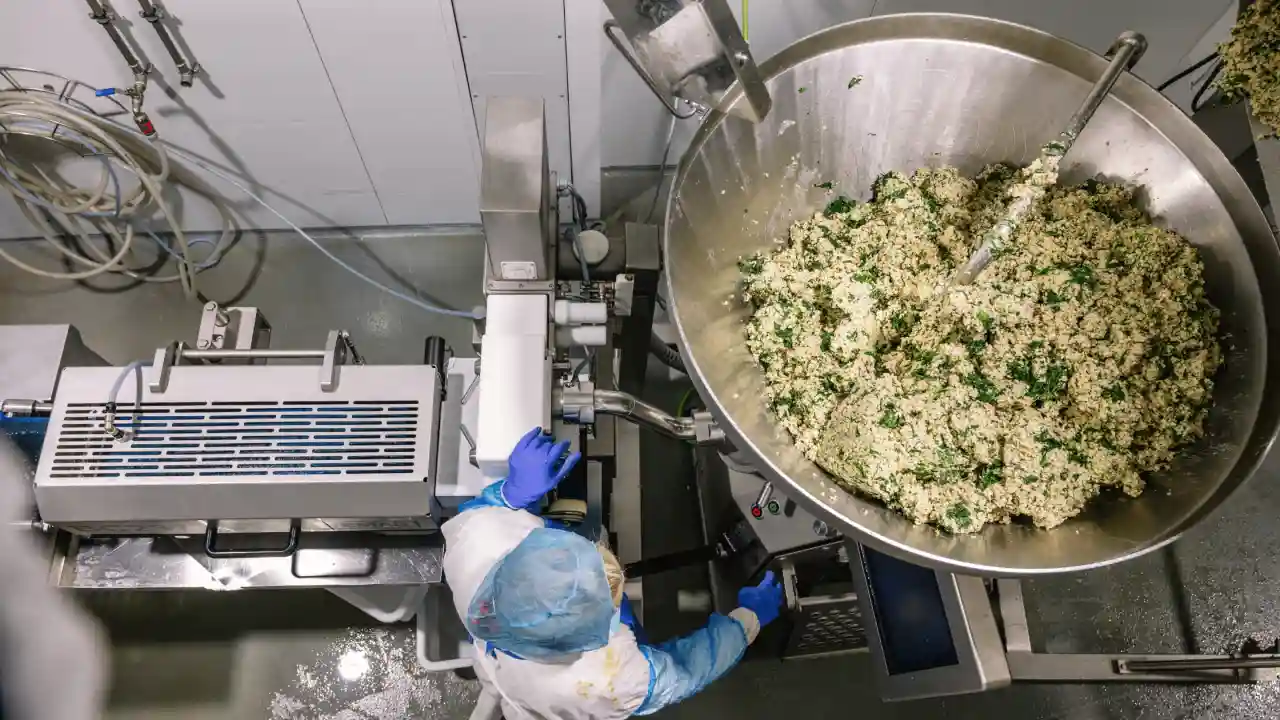
Where thermal treatment is critical, manufacturers verify that the required conditions are achieved. For example, in the production of croquettes, controls may confirm that the product reaches the required core temperature during frying.

In dry extrusion processes, moisture monitoring helps ensure that the product is sufficiently dehydrated to meet its specifications.

These controls are not managed in isolation, but as part of a previously validated process monitored by the relevant teams.

Packaging, Sealing and Storage

Once the product has been manufactured, packaging and storage conditions become critical for maintaining safety and stability.

Depending on the product, different storage requirements and control measures may apply. These are complemented by finished product testing and shelf-life studies, which help assess how the product performs throughout its intended shelf life.

How to Ensure Food Safety in Custom Plant-Based Projects

When developing a product for a specific customer, food safety must be integrated from the earliest stages of the project. It is not simply about controlling the finished product, but about verifying that the proposed formulation and manufacturing process are suitable for industrial-scale production.

Designing Safe and Stable Formulations

Development begins with a formulation and manufacturing process designed around the characteristics of the final product. At this stage, the Quality team is also involved, reviewing and validating the procedures and controls before moving production to the factory floor.

This collaboration helps identify specific control requirements before manufacturing begins and ensures that suitable procedures are established for the product.

Industrial Validation Before Launch

Industrial validation is an important step in confirming that a product developed during earlier stages can be reproduced under real manufacturing conditions.

Before production begins, established procedures and controls are reviewed, and the corresponding checks are carried out during manufacturing. Finished product analysis and shelf-life studies, typically performed by external laboratories, complete the validation process.

The objective is to ensure that the product not only works at laboratory scale but can also be manufactured consistently and reliably under industrial conditions.

Adapting to the Customer, Distribution Channel and Final Format

Every product has different requirements depending on its formulation, format and storage conditions. As a result, food safety controls must be defined according to the specific characteristics of each project.

This is particularly important in bespoke developments, where raw materials, manufacturing processes, packaging formats and storage conditions may all vary.

Plant-Based Food Safety Regulations, Traceability and Control Systems

In addition to manufacturing controls, structured management and traceability systems help maintain control throughout the entire supply chain.

Traceability of Ingredients and Batches

Traceability makes it possible to follow a product from its raw materials through to delivery to the customer. It is considered a fundamental aspect of food safety because it enables the identification of the origin and movement of products across the supply chain.

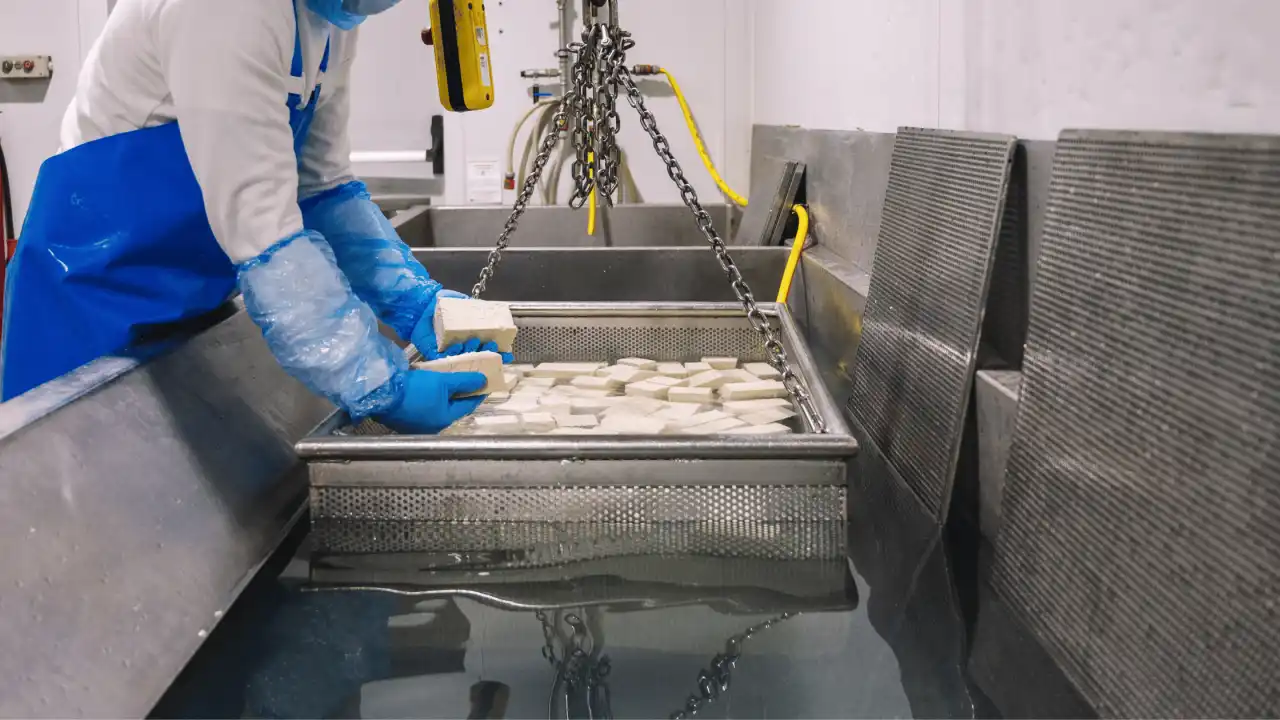
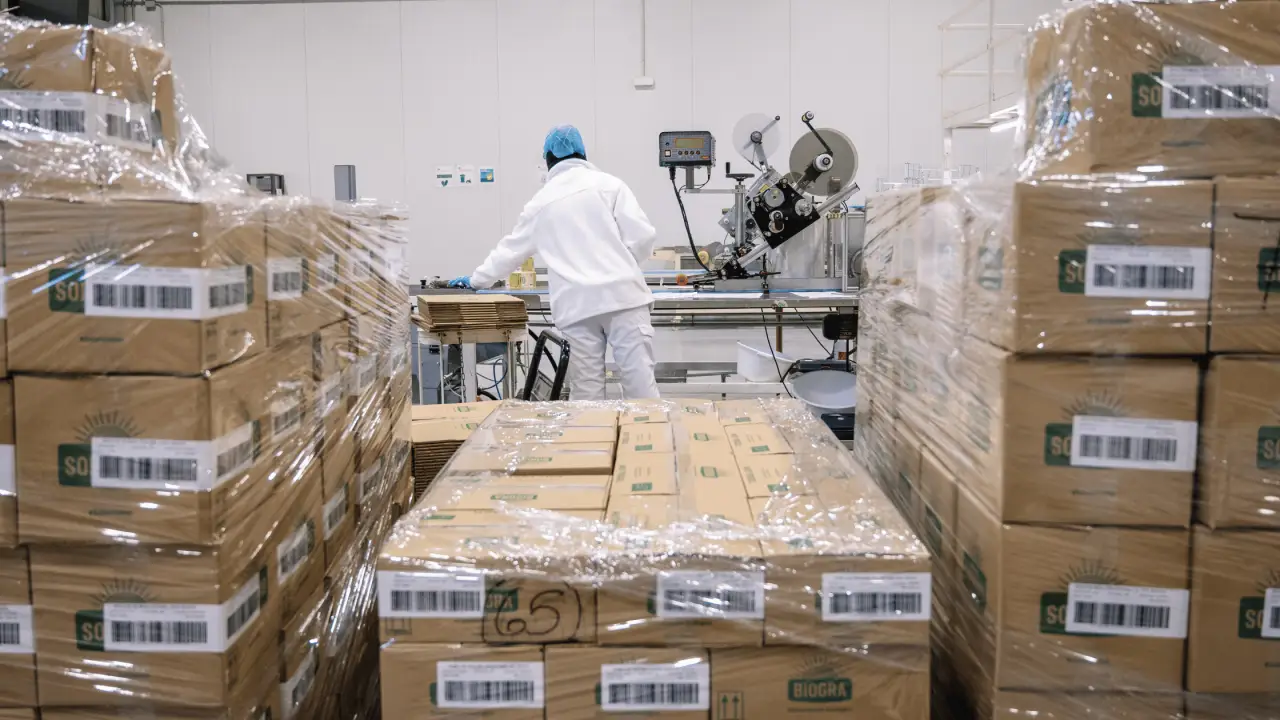
At Sanygran, products can be traced from the delivery documentation of the raw materials used in production through to the customers who received the corresponding batch. This provides full visibility of each production run and supports rapid action should an issue arise.

Quality Controls and Document Verification

Food safety relies on both physical and analytical controls and the documented procedures that support them.

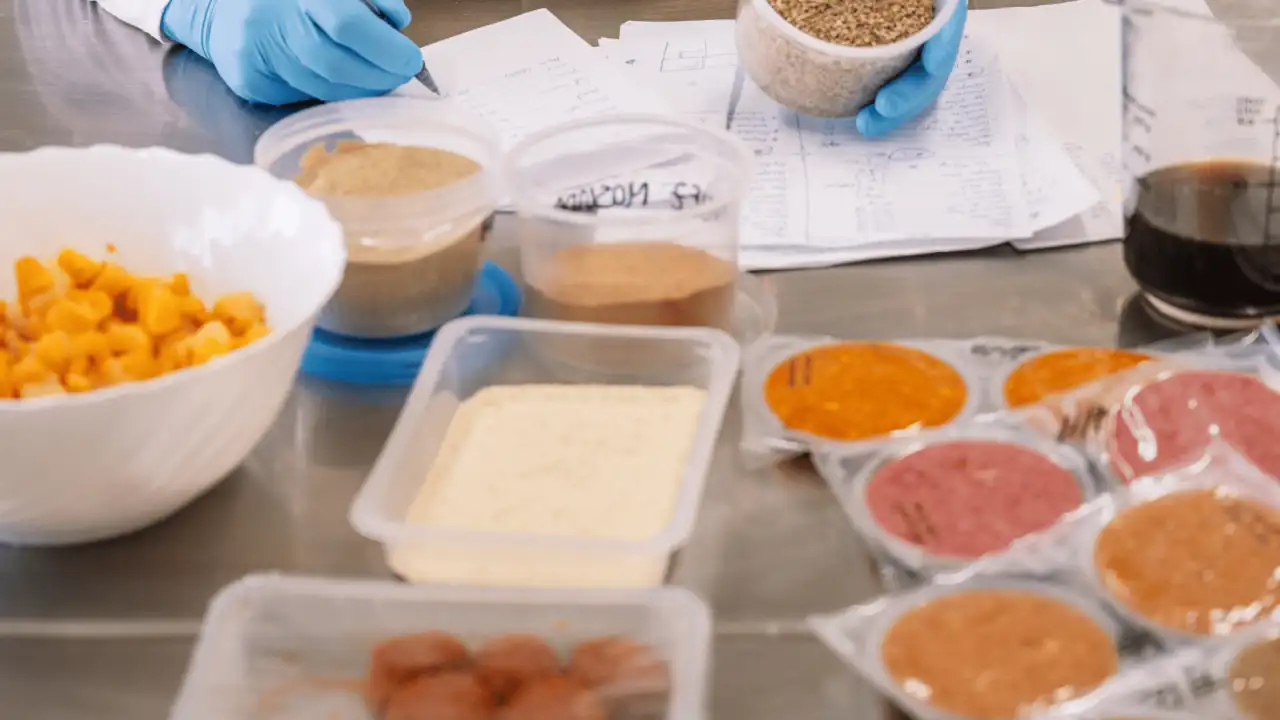
Microbiological testing, metal detection, in-process verification and finished product analysis all form part of this system. The specific controls required depend on the characteristics and risks associated with each product.

Allergen management also requires dedicated procedures. When a product containing an allergen is manufactured before a product that must be free from that allergen, a thorough cleaning process is carried out between productions. Verification activities, such as gluten testing at different points along the production line, help confirm the absence of the allergen.

Audits and Supplier Approval

Food safety also depends on maintaining controlled and verifiable procedures. Supplier approval programmes and audits form part of a system designed to evaluate and maintain standards throughout the supply chain.

In this context, manufacturing facilities certified under the IFS Food standard provide additional assurance for customers. IFS Food assesses products and production processes to verify a manufacturer’s ability to produce food that is safe, authentic and of consistent quality while meeting legal requirements and customer specifications.

At Sanygran, all production facilities are IFS-certified, helping support customer approval processes and third-party audits.

Plant-Based Food Safety, Scalability and Industrial Viability

Food safety is directly linked to the ability to manufacture a product consistently at industrial scale. A product that performs well during laboratory testing must also be capable of being reproduced under controlled industrial conditions.

Batch-to-Batch Consistency and Process Repeatability

Defining specific parameters and controls for each product helps reduce variability between batches and maintain the characteristics established during development.

This is one of the reasons why involvement from the Quality team throughout the project is important. Their participation helps ensure that procedures are reviewed before production begins and that they are correctly implemented during manufacturing.

Reducing Waste, Incidents and Returns

A well-defined control system helps identify deviations before they become product issues. This can contribute to reducing waste, rework and production incidents, ultimately improving manufacturing stability and efficiency.

For customers that require a reliable supply, the ability to manufacture safely and consistently is just as important as achieving the desired sensory characteristics.

What Does a Specialised Plant-Based Supplier Contribute?

Food safety should not be viewed as a control activity separate from product development. Instead, it should be considered an integrated part of the entire manufacturing process.

At Sanygran, controls are adapted to the characteristics of each product and process, covering raw materials, manufacturing parameters, finished products, shelf life, allergen management and traceability. The involvement of the Quality team from the early stages of development helps ensure that projects move to production with procedures that have already been reviewed and validated.

This is supported by the IFS certification of all production facilities and a traceability system capable of following each production run from the raw materials used through to the customers who receive it.

Because developing a plant-based product is not only about creating an effective formulation. It is also about being able to manufacture it safely, control it consistently and reproduce it reliably when production scales up.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

The Importance of Validating Plant-Based Production

The Importance of Validating Plant-Based Production

  • Validating plant-based production means checking that formulation and process work together, not just that the prototype performs well in the laboratory.
  • Validation reduces risks before industrialization: it helps detect issues in texture, flavor, stability, shelf life, food safety, waste, costs, and scalability.
  • The process should move through stages: laboratory, pilot plant, and industrial batch, involving R&D, quality, production, and procurement to ensure repeatability.

The importance of validating plant-based production lies in ensuring that a formulation not only works in the laboratory, but can also be manufactured in a safe, stable and repeatable way at industrial scale.

When developing a new product, moving from a prototype to a production line introduces new variables, including equipment, processing times, raw materials, manufacturing conditions and packaging systems. What performs well in a controlled trial may not necessarily behave in exactly the same way when production is scaled up.

For this reason, validation acts as the bridge between development and manufacturing, making it possible to verify that the product maintains its intended characteristics in terms of texture, flavour, stability, yield and shelf life before moving towards stable industrial production.

What Does It Mean to Validate Plant-Based Production in an Industrial Environment?

Validating plant-based production means confirming that the formulation and the manufacturing process work together to consistently deliver the intended product under real production conditions.

The objective is not simply to create a sample that meets expectations. The real challenge is being able to reproduce that result batch after batch, within predefined specifications.

Validation of Formulation and Product Performance

Formulation validation allows manufacturers to assess how a product performs under the real conditions for which it has been designed.

Depending on the application, parameters that may be evaluated include:

  • Texture and bite.
  • Moisture content.
  • Cohesion.
  • Yield.
  • Stability.
  • Cooking performance.
  • Sensory profile.

Evaluation does not necessarily end once manufacturing is complete. Depending on the product, additional testing may include cooking trials, regeneration tests, application trials and assessments under chilled or frozen storage conditions.

The goal is to confirm that the product not only achieves the desired characteristics immediately after production, but also performs as expected throughout its lifecycle.

Validation of the Manufacturing Process

A formulation may be correctly designed and still require adjustments when transferred to production.

Stages such as mixing, cooking, cooling, forming and packaging can all influence the final result.

For this reason, validation must confirm that the parameters established for each production stage consistently reproduce the desired product characteristics.

Why Validation Is Critical Before Industrialisation?

Validation helps reduce uncertainty before committing resources and production capacity at full scale.

The earlier a deviation is identified, the easier it is to determine its cause and implement corrective actions.

Reducing Technical and Food Safety Risks

Validation trials help identify potential product and process deviations before they affect routine manufacturing.

They can help detect:

  • Stability issues.
  • Deviations from specifications.
  • Unexpected process behaviour.
  • Storage-related issues.

Differences caused by changes in raw materials or manufacturing conditions.

Some issues only become apparent when products are exposed to real storage and distribution conditions. Changes in texture, flavour, appearance or stability may require modifications to the formulation or process before industrialisation can proceed.

Impact on Costs, Waste and Scalability

Insufficient validation can generate costs that were not anticipated during development.

Frequent process adjustments, production waste, out-of-specification batches and delayed product launches are just some of the challenges that can arise when a formulation has not been properly validated.

Scaling up should make it possible to move from laboratory testing to industrial production without losing the characteristics defined for the final product.

This is one of the biggest challenges in product development. A factory is not simply a larger laboratory. Equipment, batch sizes and process conditions are different, and it is essential to understand how the formulation performs under these new circumstances.

Technical Aspects That Should Be Validated in Plant-Based Products

Not all products require validation of exactly the same parameters. The validation plan should be adapted to the technology, formulation and intended application.

Texture, Flavour and Sensory Performance

Sensory characteristics play a major role in the acceptance of any food product.

For this reason, validation may include assessment of:

  • Texture.
  • Bite.
  • Juiciness.
  • Flavour intensity.
  • Aftertaste.
  • Appearance.
  • Batch-to-batch consistency.

At Sanygran, sensory evaluations form part of the different stages of product development. Laboratory trials and industrial trials are assessed before samples are sent to customers, allowing potential adjustments to be identified in advance.

Sensory evaluation should also extend beyond the production day. Depending on the product and its intended shelf life, it is important to understand how these characteristics evolve during storage.

Stability, Preservation and Shelf Life

Validation must also determine whether a product maintains its characteristics throughout its intended shelf life.

This may include evaluation of:

  • Quality evolution.
  • Microbiological stability.
  • Physical stability.
  • Texture retention.
  • Sensory profile evolution.
  • Shelf life.

For chilled products, shelf life can become one of the most demanding aspects of development. It is not enough to achieve excellent texture and flavour on the day of manufacture. These characteristics must remain within defined specifications throughout the intended commercial life of the product.

Compatibility with Packaging and Distribution

Packaging and logistics conditions also contribute to overall product performance.

The selected packaging system must be compatible with the characteristics of the food and with the intended storage and distribution conditions.

For this reason, validation should consider the product exactly as it will reach the market, taking into account packaging format, storage conditions, transport and handling.

How Is Plant-Based Production Validated Step by Step?

Validation is generally carried out progressively, moving from controlled tests to conditions that increasingly resemble real manufacturing environments.

Laboratory Testing and Prototyping

The laboratory is the starting point for adjusting formulations and evaluating the first product versions.

During this phase, manufacturers may assess:

  • Raw material functionality.
  • Texture.
  • Sensory profile.
  • Stability.
  • Formulation behaviour.

Laboratory trials help eliminate unsuitable options and optimise formulations before moving to a larger scale.

However, a formulation validated in the laboratory cannot yet be considered ready for industrial production.

Pilot or Pre-Industrial Trials

The next step is to reproduce manufacturing conditions in an environment that more closely resembles industrial production.

This stage makes it possible to assess how factors such as equipment, production volumes, processing times and operating conditions influence the product.

It is common for adjustments to emerge during this phase that were not evident during laboratory testing. Identifying them at this stage allows formulation or process modifications to be made before full-scale production.

Validation of Industrial Batches

Industrial trials allow manufacturers to evaluate product performance under the actual conditions in which it will be produced.

This stage typically assesses:

  • Process repeatability.
  • Compliance with specifications.
  • Product consistency.
  • Formulation performance at industrial scale.
  • Sensory results.

Once this phase has been successfully completed, manufacturers have a much stronger basis for defining production conditions and moving towards stable manufacturing.

Which Departments Should Be Involved in Validation?

Validation is not the responsibility of a single department. Successful industrialisation requires input from multiple areas of the business.

R&D, Quality and Production

Each department plays a different role within the validation process:

  • R&D works on formulation and product performance.
  • Quality verifies compliance with specifications and requirements.
  • Production evaluates process feasibility and repeatability within the factory.

Collaboration between these areas helps identify deviations earlier and supports better decision-making through a broader understanding of the product.

In certain projects, other departments such as marketing and sales may also participate, particularly when the product needs to be assessed against project objectives or customer expectations.

Purchasing and Product Development

Raw materials and their availability can also influence industrialisation.

For this reason, development teams should consider:

  • Availability of raw materials.
  • Technical specifications.
  • Cost.
  • Supply consistency.
  • Alternative sourcing options.

A technically viable formulation must also be realistic from both a production and supply perspective.

Common Mistakes When Validation Is Not Performed Properly

Failing to adequately validate a formulation can allow relatively small issues to become major problems once the product reaches production or the market.

Scaling Up Without Reproducibility

One of the most common mistakes is assuming that a formulation that performs well in the laboratory will behave exactly the same way in production.

As scale increases, differences related to:

  • Equipment.
  • Batch volumes.
  • Processing times.
  • Raw materials.
  • Manufacturing parameters.
  • can begin to appear.

If these variables have not been properly evaluated, maintaining consistent production and controlling deviations becomes significantly more challenging.

Failing to Adapt the Product to the Sales Channel

A product should be validated according to how it will ultimately be used and marketed.

Storage conditions, distribution requirements, preparation methods and consumption patterns can vary depending on the application and sales channel.

For example, a chilled retail product must maintain its characteristics throughout its intended shelf life and withstand normal distribution and storage conditions.

For this reason, validating a product also means validating the environment in which it will exist.

How Does Sanygran Add Value to This Validation Process?

Validation becomes more effective when approached from a broader perspective that includes the product, the process and the final application.

Tailor-Made Development Based on Customer Specifications

At Sanygran, we work with a range of plant-based ingredients and solutions, adapting developments to the requirements of each project.

Depending on the application, variables that may be adjusted include:

  • Formulation.
  • Texture.
  • Format.
  • Flavour intensity.
  • Structure.
  • Manufacturing technology.

Before samples are sent to customers, internal testing is carried out to verify that results meet the defined objectives.

Sensory evaluations help assess characteristics such as texture, bite, flavour intensity and aftertaste, both during laboratory trials and after industrial validation.

Support Throughout Testing, Optimisation and Scale-Up

The transition from laboratory development to production is not always straightforward. During testing, small deviations may appear that require changes to raw materials, formulation adjustments or modifications to processing parameters.

Having a team capable of assessing these variables together helps facilitate decision-making and supports the move towards more stable manufacturing.

Ultimately, validating plant-based production is not simply about proving that a product works once. It is about demonstrating that it can be manufactured safely and consistently while maintaining the characteristics defined for the product over time and at industrial scale.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

Better Repeatability in Plant-Based Products with Multifunctional Ingredients

Better Repeatability in Plant-Based Products with Multifunctional Ingredients

  • Repeatability is critical in plant-based products, because small variations in texture, moisture, cohesion, or cooking performance can cause deviations, waste, and production adjustments.
  • Multifunctional ingredients help create more robust formulations, combining structure, water retention, cohesion, texture, and stability within a single technological solution.
  • Improvement depends on formulation, process, and industrial validation, assessing raw materials, moisture, mixing, heat treatment, shelf life, safety, labeling, and batch-to-batch scalability.

Achieving better repeatability in plant-based products with multifunctional ingredients is one of the key challenges faced by R&D, quality and production teams when a formulation moves from the laboratory to industrial manufacturing.

In production, it is not enough for a recipe to work once. It must perform in a consistent, scalable and predictable way, even when small variations occur in raw materials or processing conditions.

In this context, multifunctional ingredients can help create more robust formulations that fulfil several technological functions within the same product. However, their selection should always be based on the requirements of the final application and the manufacturing process.

Why Is Repeatability Critical in Plant-Based Formulations?

Repeatability is the ability to produce a product with consistent characteristics across different production runs.

In plant-based products, small variations can affect parameters such as texture, moisture, cohesion, yield and cooking performance. When these differences accumulate, deviations from specification may occur, requiring adjustments during production.

For this reason, an industrial formulation should be designed not only to deliver a good product, but also to maintain its characteristics consistently from batch to batch.

Impact on Quality, Yield and Waste

A seemingly small variation can have significant consequences in production.

For example, a difference in the water absorption capacity of a raw material may alter the final weight, texture or juiciness of a formulation. If this behaviour is not properly controlled, process adjustments, product rejections or waste levels may increase.

Repeatability helps maintain more predictable production parameters and allows quality and production teams to keep products within defined specifications.

Risks for Scale-Up and Industrial Standardisation

A formulation validated at laboratory scale does not always behave in exactly the same way once transferred to production.

Scaling up introduces new variables, including different mixing equipment, processing times, production capacities and operating conditions. These factors are compounded by the natural variability that can exist between raw materials.

For this reason, development should consider from the outset how a formulation will perform under real manufacturing conditions. Industrial validation is essential for identifying potential deviations before a product reaches routine production.

What Do Multifunctional Ingredients Bring to a Formulation?

A multifunctional ingredient is one that can perform more than one function within a formulation, contributing to different characteristics of the final product.

In plant-based applications, this functionality can be particularly beneficial when the goal is to simplify a recipe or ensure that certain attributes rely on a more controlled ingredient system.

The objective is not simply to reduce the number of ingredients, but to select those that deliver genuine technological value to the application.

Technological Functions They Can Integrate

Depending on their nature and the formulation in which they are used, some ingredients may contribute to several functions, including:

  • Structure development.
  • Water retention.
  • Cohesion.
  • Texture.
  • Stability.
  • Performance during thermal processing.

For example, certain plant-based texturates can provide both structure and texture while also contributing to water management within a formulation.

This combination can be especially useful in applications such as plant-based burgers, fillings, sauces and prepared meals, where multiple attributes need to remain balanced.

Advantages Compared with Systems Using Many Ingredients

A formulation built around ingredients capable of delivering several functions can simplify various aspects of development and production.

It may help streamline the recipe, reduce unnecessary ingredient interactions and facilitate process control. It can also simplify the management of raw materials and specifications.

However, simplifying a formulation does not always mean using fewer ingredients. The priority should be to achieve the right balance between functionality, cost, processing requirements and final product characteristics.

Formulation Variables That Most Affect Repeatability

Repeatability does not depend solely on selecting the right ingredient. It is the result of the interaction between raw materials, formulation and manufacturing processes.

Raw Materials, Moisture and Functional Performance

The characteristics of raw materials may vary and influence formulation performance.

Parameters such as moisture content, particle size, water absorption capacity and functional behaviour can affect the final result and must be considered during development.

For example, two raw materials with a similar composition may perform differently during mixing, hydration or thermal processing.

This is why working with clear specifications and selecting suitable raw materials for each application helps minimise variability from the start.

Interaction Between Ingredients and Process

Formulation cannot be analysed independently from processing conditions.

Variables such as temperature, mixing time, mixing intensity and ingredient addition order can alter the behaviour of the same recipe.

As a result, achieving a repeatable product requires defining not only which ingredients to use, but also how they should be processed and under which conditions.

How Multifunctional Ingredients Help Stabilise Plant-Based Production

When an ingredient consistently performs several functions, it can contribute to more robust formulations and facilitate process control.

The objective is to reduce the formulation’s sensitivity to small variations and achieve more predictable manufacturing performance.

Improved Control of Texture, Viscosity and Structure

Depending on the application, ingredients such as plant-based texturates, protein concentrates and certain functional starches can help control multiple formulation properties.

In a specific application, for example, a texturate may provide structure while contributing to water retention, whereas other ingredients help adjust cohesion or viscosity.

The key is finding the right combination so that each ingredient fulfils a defined role without creating imbalances within the formulation.

Greater Tolerance to Process Variations

A well-designed formulation can provide greater resilience to the small variations that routinely occur in production.

This does not mean that multifunctional ingredients eliminate variability entirely, but rather that a properly optimised formulation can be more robust and facilitate process standardisation.

For this reason, plant validation remains essential before a formulation is considered ready for routine manufacturing.

Technical Criteria for Choosing a Multifunctional Ingredient to Improve Plant-Based Repeatability

Ingredient selection should start with the final application and the real production conditions under which the product will be manufactured.

Not all ingredients behave the same way in every matrix, nor do they provide the same advantages in every process.

Compatibility with the Matrix and the Process

Before incorporating a multifunctional ingredient, its compatibility with the following aspects should be assessed:

  • The formulation.
  • The manufacturing process.
  • Available equipment.
  • Thermal treatment.
  • Storage conditions.

In industrial development, these variables must be evaluated together. An ingredient may deliver excellent technological performance but still not be the most appropriate option for a specific production line or application.

Impact on Shelf Life, Safety and Labelling

Technological functionality is only one of the selection criteria.

It is also important to assess how the ingredient influences product stability, shelf life, food safety requirements and final labelling.

For industrial development, the most suitable solution is the one that balances all these factors without compromising performance or manufacturing feasibility.

Sanygran, Multifunctional Solutions for More Repeatable Plant-Based Production

At Sanygran, we work with a range of plant-based ingredients and solutions, including plant-based texturates, pea protein concentrates and solutions such as Legumeat®, adapting their use to the requirements of each development project.

The combination of formulation expertise, process knowledge and industrial validation helps identify the variables that have the greatest impact on product performance and optimise them before moving into routine production.

The objective is not to create a formulation that works only once, but a solution that can be consistently reproduced at industrial scale, maintaining the characteristics defined for the final product.

Because in plant-based manufacturing, the real test of a successful formulation is its ability to deliver the same result again and again.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

The Importance of Texture in Plant-Based Products

The Importance of Texture in Plant-Based Products

  • Texture defines the acceptance of a plant-based product, especially in meat analogues, because it determines bite, juiciness, cohesion, fibrousness, and the eating experience.
  • There is no universal texture: each application —chicken-style bite, burger, tofu, hummus, or prepared meal— requires a structure adapted to its final use.
  • Texture is built through raw materials, formulation, and process, and must be validated in the laboratory, industrial production, shelf life, cooking, and reheating to ensure repeatability.

The importance of texture in plant-based products goes far beyond mouthfeel. In categories such as meat alternatives, achieving the right structure, bite and juiciness can make the difference between a product that performs well in an initial trial and one that becomes part of a consumer’s regular shopping basket.

However, there is no single texture that works for every application. A chicken-style plant-based piece requires a specific structure and bite, while a plant-based burger, tofu or hummus each have completely different requirements.

For this reason, developing the right texture involves working with raw materials, formulation and manufacturing processes together, always considering how the product will be consumed and what performance is expected from the final application.

Why Does Texture Influence the Success of a Plant-Based Product?

Texture is one of the key attributes that defines the eating experience of a plant-based product.

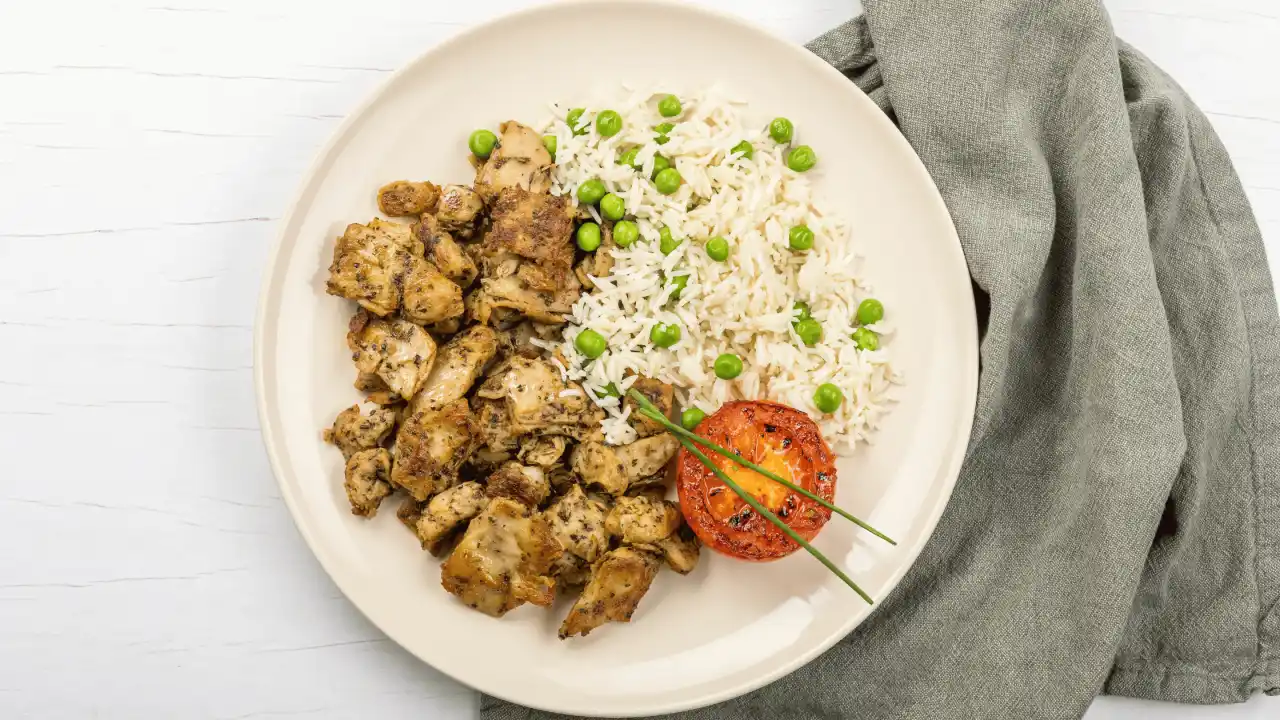
In categories such as plant-based chicken-style chunks, a structure that is too soft, overly compact or insufficiently defined can move the product away from the experience consumers expect. On the other hand, a well-developed texture can provide a more satisfying bite and a structure that matches the intended application.

The same principle applies to other product categories. A plant-based burger may require a compact yet juicy matrix; tofu may need firmness and elasticity; while hummus should deliver a smooth and creamy texture.

This demonstrates that a texture that works perfectly in one application may not work in another.

In addition, texture affects more than just the final eating experience. It also influences industrial factors such as:

  • Product handling.
  • Performance during cooking.
  • Resistance during packaging.
  • Integration into prepared meals.
  • Stability during storage.
  • Consistency between batches.

For this reason, texture should be defined during the earliest stages of product development and validated under real manufacturing and consumption conditions.

Which Texture Attributes Are Critical in Plant-Based Formulation?

The attributes that need to be prioritised depend on the product and the experience being targeted. Some of the most important parameters in plant-based product development include the following.

Firmness

Firmness determines the resistance a product offers during handling and consumption.

For example, tofu may require a firm and stable structure to facilitate cutting and handling. In other products, excessive firmness might create an unpleasant eating experience.

The objective is not simply to make a product firmer, but to achieve the appropriate level of firmness for each application.

Juiciness

Juiciness is particularly important in products designed to replicate foods of animal origin, such as burgers or chicken-style chunks.

A structure that can manage moisture effectively may contribute to a juicier eating experience. However, the challenge is always to balance moisture and structure to maintain product stability.

Cohesion

Cohesion ensures that the different components of the matrix remain bound together.

This attribute is particularly important in products that need to withstand handling, cutting, packaging or cooking. Insufficient cohesion can result in breakage or fragmentation, while an excessively compact structure may negatively affect mouthfeel.

Bite

Bite describes how a product responds during chewing and is especially important in the development of meat analogues.

In a plant-based chicken-style chunks, for example, developers may seek an initial resistance followed by a pleasant chewing experience. The final result depends on the raw materials, formulation and manufacturing technology used.

Fibrousness

Fibrousness is one of the most valuable texture attributes when developing products such as chicken-style chunks produced using high-moisture technology.

This technology makes it possible to work with protein structures at different levels of organisation, creating products with textures tailored to specific applications.
Size, structure, bite and cooking performance must all be developed together.

Creaminess

Not all plant-based applications require a fibrous structure or pronounced bite.

For products such as hummus, the target texture is entirely different. Creaminess, uniformity and the absence of graininess are among the attributes that influence quality perception.

This reinforces an important principle: texture should always be developed with the final application in mind.

How Is Texture Built in Industrial Processes?

The final texture of a plant-based product is the result of multiple interacting variables. It does not depend solely on selecting a specific protein or ingredient, but on how raw materials, formulation and manufacturing processes work together.

Ingredient Selection and Functionality

Each raw material offers specific functional characteristics and may influence structure, water retention, cohesion and mouthfeel.

At Sanygran, we work with a range of raw materials including soy and pea proteins, as well as other ingredients used in certain developments, such as gluten and oats.

The choice depends on the intended result. Different combinations of raw materials can also be used to adjust product characteristics according to the application.

For high-moisture chunks, ingredient selection becomes particularly important because composition and process conditions must work together to achieve the desired structure.

Process Parameters That Alter Texture

Even a well-designed formulation can deliver different results if manufacturing conditions change.

Variables such as temperature, moisture, pressure, processing time, shear forces and cooling conditions can significantly influence the structure obtained.

This is especially relevant in high-moisture extrusion, where process control enables developers to create different texture profiles depending on the target application.

At Sanygran, production parameters are adjusted according to factors such as raw material selection, product size, texture requirements and target sensory characteristics, helping to achieve results that can be reproduced consistently at industrial scale.

Texture and Shelf Life: Balancing Stability and Sensory Quality

A suitable texture should not be evaluated solely at the point of manufacture.

A product must maintain its characteristics throughout storage, distribution, handling and, when applicable, cooking or reheating.

The Effect of Packaging and Distribution on Texture

Preservation systems and distribution conditions can influence the behaviour of plant-based products.

Changes in moisture, temperature and storage conditions may affect attributes such as firmness, cohesion and juiciness.

For this reason, product development should consider the final format and storage conditions from the outset, particularly for solutions intended for retail or industrial applications.

How to Validate Texture Stability During Shelf-Life Testing

Texture should form part of any shelf-life validation programme.

Depending on the application, factors that may be assessed include:

  • Retention of firmness.
  • Structural stability.
  • Evolution of bite.
  • Performance after freezing and thawing.
  • Response during cooking or reheating.
  • Consistency between batches.

At Sanygran, in addition to laboratory testing, we carry out industrial-scale trials and sensory evaluations to verify that products meet the required criteria and to generate useful data when determining shelf life.

Texture and the Eating Experience in Plant-Based Applications

Texture should be designed around the intended use of the product and the eating experience it is expected to deliver.

Adapting Texture to Product Format

There is no universal texture for plant-based products.

A chicken-style piece may require a fibrous structure and a defined bite. A burger may require a compact and juicy matrix. Tofu may need firmness and elasticity, while hummus demands a smooth and creamy texture.

At Sanygran, we work with different sizes, structures, raw materials and flavour profiles, adapting these variables to each specific application.

For ingredients produced through high-moisture extrusion, for example, we can create different sizes, from smaller formats to the more common bite-sized chunks, depending on the intended use.

These products can be incorporated into ready meals, bowls, salads, wraps and sauces, or marketed directly in trays for consumers to use as they wish.

Texture Performance During Cooking and Reheating

Products must maintain their intended performance throughout normal use.

Depending on the application, it may be necessary to evaluate how they respond to cooking, reheating, regeneration or integration into other food preparations.

For a chicken-style piece, for example, it is not enough to achieve the right texture when cold. The structure and bite must also remain consistent after the intended preparation method.

For this reason, development trials should replicate, as closely as possible, the conditions the product will experience after commercialisation.

How to Evaluate and Control Texture During Product Development

Developing the right texture requires more than achieving a successful first prototype. The result must be compared, refined and validated until it becomes a reproducible industrial solution.

Sensory and Instrumental Indicators

Sensory evaluation allows developers to assess attributes that cannot always be captured through a single measurement.

At Sanygran, we perform internal tastings during both laboratory trials and industrial-scale testing before samples are sent to customers.

These evaluations involve different departments, including R&D, Quality and Marketing/Commercial teams.

Attributes typically assessed include:

  • Texture.
  • Bite.
  • Flavour intensity.
  • Aftertaste.
  • Juiciness.
  • Appearance.
  • Suitability for the intended application.

This collaborative approach helps identify potential issues before products reach the customer sample stage.

Quality Criteria for Scaling Without Losing Texture

One of the biggest challenges in industrial development is maintaining the texture achieved during initial trials when production is scaled up.

Raw materials may vary, while manufacturing conditions can differ between equipment or production volumes. As a result, maintaining consistency requires careful control and standardisation of the variables that affect texture.

Industrial experience is particularly important at this stage: it is not enough to achieve the desired texture in the laboratory; it must also be reproducible in full-scale production.

Common Challenges When Developing Texture in Plant-Based Products

Achieving the desired texture often requires multiple development iterations. Small changes in formulation or processing can significantly affect the final result.

How to Correct Unstable or Inconsistent Textures?

When texture does not meet expectations, the entire process needs to be reviewed.

This may include evaluating:

  • Raw materials.
  • Ingredient ratios and combinations.
  • Processing conditions.
  • Product size and structure.
  • Post-processing treatments.
  • Storage conditions.

The objective is not to make isolated changes, but to identify which variable is genuinely influencing the result.

For example, a structure that performs well in a bowl application may not behave in the same way when incorporated into a sauce or prepared meal. In such cases, texture adjustments may be required to suit the new conditions of use.

What to Consider When Working with Tailor-Made Solutions?

Every application has its own requirements.

At Sanygran, we can work with different raw materials, sizes, textures and flavour profiles, adapting development to the specific needs of each product.

This flexibility is particularly useful when a company needs a solution that fits a particular product concept, manufacturing process or commercial format.

The key is first understanding what the product needs to do, and then defining the texture, structure and behaviour required to achieve that goal.

Sanygran, a Technical Partner for Optimising Texture in Plant-Based Products

Texture is the result of combining raw materials, formulation, technology and manufacturing processes.

At Sanygran, we develop plant-based solutions with particular expertise in high-moisture chunks, adapting variables such as size, structure, texture and flavour according to the application and project requirements.

Development combines laboratory testing, industrial validation and sensory evaluation to assess texture, bite, flavour intensity and aftertaste before samples are submitted to customers.

Because in plant-based products, there is no single texture that works for every application. Each product requires specific characteristics and a manufacturing process capable of reproducing them consistently.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

How Is Hydration Managed in Industrial Processing?

The Importance of Hydration in Plant-Based Products

  • Hydration is critical in dry plant-based texturates, because it determines bite, juiciness, cohesion, stability, and finished-product yield.
  • It is not about adding more water, but the right amount: raw material, format, fibers, starches, mixing, temperature, and timing all affect absorption and retention.
  • It must be validated under real industrial conditions, as scale-up can alter water distribution, final texture, batch-to-batch uniformity, and shelf life.

The importance of hydration in plant-based products becomes especially evident when working with dry plant-based texturates, as water management has a direct impact on texture, juiciness, cohesion and the overall performance of the finished product.

However, hydrating a texturate is not simply a matter of adding water. The amount of water available, absorption time, raw material selection and formulation characteristics all determine how the ingredient will behave once incorporated into the final product.

In this article, we explore how water is managed in dry plant-based texturates, which factors influence hydration, and why this process is critical for both product development and industrial-scale manufacturing.

Why Is Hydration Critical in Plant-Based Formulations?

Dry plant-based texturates need to absorb water in order to develop the functional properties they will later contribute to the finished product.

The amount of water absorbed and the ingredient’s ability to retain it can influence characteristics such as bite, juiciness, cohesion and formulation stability.

For this reason, hydration should be considered a key technological variable in plant-based product development, alongside raw material selection, formulation design and processing conditions.

Furthermore, water management begins long before the final formulation stage. In the case of dry texturates, there is an initial manufacturing phase during which the ingredient’s moisture content is reduced through controlled drying to ensure stability and suitability for storage. Later, when incorporated into a formulation, the texturate reabsorbs water to develop the required structure and functionality.

Relationship Between Hydration, Structure and Product Behaviour

When a dry texturate absorbs water, its structure changes and develops the properties required for integration into a formulation.
The amount of water incorporated and how it is distributed can affect factors such as water retention, cohesion and structural integrity within the finished product.

In a plant-based burger, for example, properly adjusted hydration helps create a more homogeneous matrix and ensures consistent performance throughout processing.

Impact of Insufficient or Excessive Hydration

Both insufficient and excessive hydration can create manufacturing challenges.

If the texturate does not absorb enough water, some particles may remain under-hydrated, reducing their ability to integrate correctly within the product matrix.

Conversely, excessive water can make it more difficult to achieve a sufficiently stable structure and may alter formulation performance during subsequent processing steps.

The goal is not to incorporate as much water as possible, but to reach the optimum hydration level for the characteristics and processing requirements of each product.

Formulation Factors That Influence Hydration

Water absorption and retention depend not only on the texturate itself but also on the other ingredients present in the formulation and the processing conditions applied.

Raw Material Type and Water Absorption Capacity

Each plant-based raw material behaves differently when exposed to water.

At Sanygran, we work with texturates produced from soy, pea and plant-based blends, including Legumeat®, which is manufactured from soy flour, bean flour and rice flour.

Differences in composition and ingredient structure can affect hydration behaviour.

Physical factors such as texturate particle size also play an important role. A fine granule and a larger-format texturate will not necessarily absorb water at the same rate or to the same extent.

For this reason, texturate selection should always take the intended application into account.

Proteins, Fibres, Starches and Other Functional Ingredients

Hydration should never be assessed in isolation.

Plant proteins, fibres, starches and other functional ingredients can influence both the amount of water available and the way water is distributed throughout the product.

This can affect properties such as viscosity, cohesion, water retention and final texture.

As a result, a hydration level that performs well in one formulation may require adjustment when the product composition changes.

How Is Hydration Managed in Industrial Processing?

In an industrial environment, managing hydration means ensuring that both the ingredient and the formulation behave consistently and predictably.

The way water is incorporated depends on the application and manufacturing process. In some developments, the texturate may be hydrated before being added to the recipe. In others, the water already present in the formulation and the processing conditions allow the ingredient to develop its required properties.

The key objective is to ensure that the system has been validated under real manufacturing conditions.

Process Parameters That Affect the Final Result

Variables such as temperature, mixing time, water availability, mixing intensity and ingredient addition sequence can all influence texturate performance.

For example, a texturate that remains in a mixture for several minutes before moving to the next production stage will not experience the same hydration conditions as one that is processed immediately after incorporation.

This is why standardising process conditions is essential to minimise batch-to-batch variation.

From Laboratory to Industrial Production

A formulation that performs well at laboratory scale may not behave identically once production is scaled up.

Equipment size, mixing capacity, processing times and manufacturing conditions can all change water distribution and therefore influence final texture.

For this reason, it is important to validate texturate performance under real production conditions before industrialising a product.

Relationship Between Hydration and Final Product Quality

Water management affects more than just the technical performance of a texturate. It can also influence attributes that are perceived in the finished product, particularly where consistency between batches is required.

Appearance and Matrix Uniformity

A uniform distribution of water contributes to a consistent product matrix. Conversely, variations in water incorporation or availability can lead to differences in appearance and structure.

This is particularly important in products where the texturate forms part of the final matrix, such as plant-based burgers, fillings and prepared plant-based meals, where uniformity is closely linked to quality perception.

Juiciness and Eating Experience

The amount of water retained within a product can also influence the perception of juiciness during consumption. However, this attribute is not determined solely by hydration level. The overall formulation, protein selection, fibres, starches and manufacturing process also contribute to the final result.

For this reason, hydration should always be evaluated alongside the other variables that define product functionality and sensory performance.

Hydration and Product Shelf Life

Moisture management is particularly important in dry plant-based texturates, as product stability depends heavily on maintaining controlled moisture levels.

Moisture, Stability and Food Safety

During dry texturate manufacturing, moisture is reduced in a controlled manner to obtain a stable ingredient suitable for storage.

At Sanygran, extrusion products are produced within controlled moisture ranges, and every batch is verified before release to ensure it complies with established quality specifications.

If the ingredient has not yet reached the target moisture level, drying continues until the required value is achieved.

This stage is essential to ensure that the texturate can be stored and transported under the intended conditions before it is incorporated into a formulation.

Sanygran: Plant-Based Texturates Adapted to Every Application

Water management does not end once the texturate has been manufactured. Its behaviour during hydration must match the requirements of the final formulation.

At Sanygran, we work with soy texturates, pea texturates and solutions such as Legumeat®, which can be used in a wide range of industrial applications, including plant-based burgers, nuggets, fillings, sauces, plant-based Bolognese products and prepared meals.

From Ingredient to Finished Product

Working with a supplier that understands both the texturate and its final application makes it easier to evaluate ingredient performance under real manufacturing conditions.

At Sanygran, we develop solutions tailored to each application, taking hydration, texture, formulation and processing requirements into account.

Because in plant-based food manufacturing, effective water management is essential for developing products that are stable, functional and capable of delivering the intended eating experience.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

Dry Plant-Based Texturates

Dry Plant-Based Texturates

  • Dry plant-based texturates provide structure, texture, and industrial functionality, enabling the development of burgers, nuggets, fillings, sauces, and prepared meals with greater formulation flexibility.
  • Texturate selection depends on the raw material, format, and final application, considering factors such as hydration, texture, flavour, yield, cost, and processing performance.
  • An industrial texturate must deliver stability, scalability, and batch-to-batch consistency, from extrusion and manufacturing through to integration into production lines and the final product.

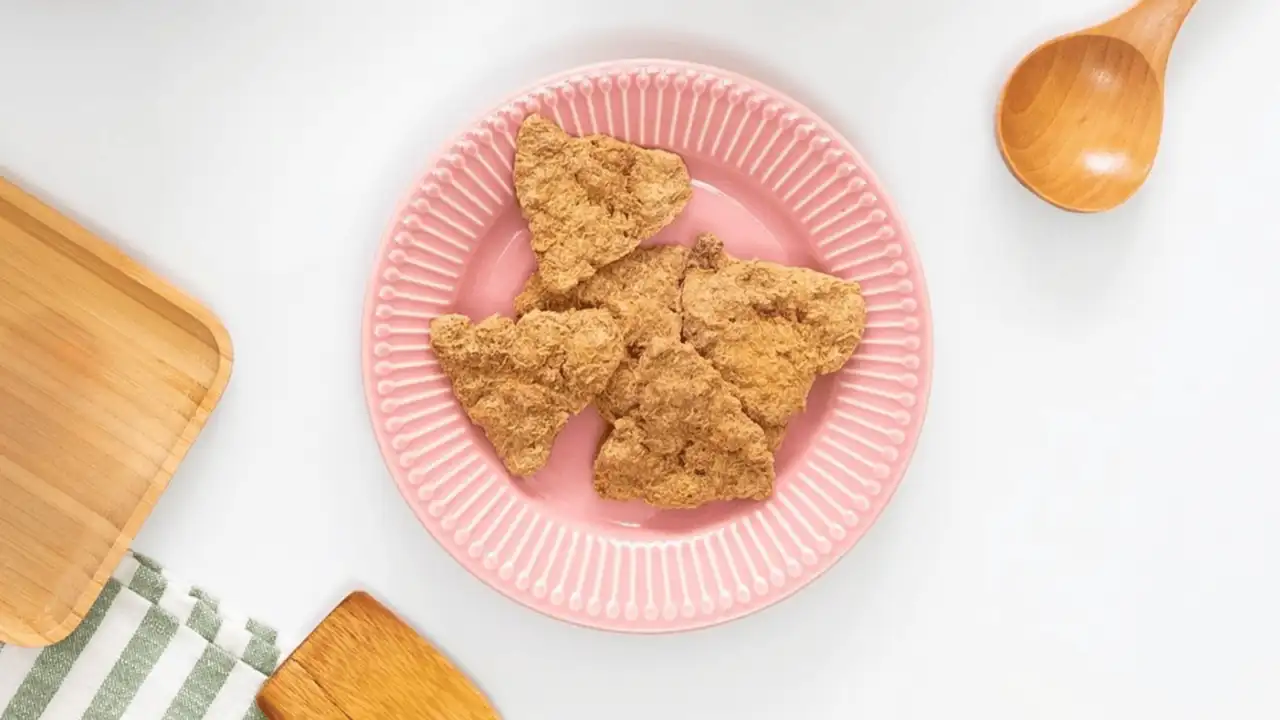
Dry plant-based texturates, commonly known as Textured Vegetable Protein (TVP), are a versatile solution for developing plant-based foods with a defined structure, reliable performance after hydration, and easy storage and transportation. Their use extends far beyond meat alternatives, as they can be incorporated into burgers, fillings, Bolognese sauces, nuggets and ready meals.

In this article, we explain what they contribute to industrial formulations, the raw materials and formats available, how they are manufactured, and the key criteria to consider when selecting a texturate for a specific application.

What are dry plant-based texturates and what role do they play in formulation?

Textured vegetable protein (TVP) are ingredients made from plant-based raw materials that, through an extrusion process, develop a structure that enables them to absorb water and create a specific texture during hydration.

For food manufacturers, their value goes beyond protein content alone. Texturates can provide structure, bite, volume and formulation integration, while also making it easier to store and handle the ingredient before it is incorporated into the final product.

Their dry format also allows manufacturers to work with a stable, easy-to-dose ingredient that can be incorporated into recipes according to the specific requirements of the finished product.

The difference between dry texturates and other plant-based matrices

Not all plant-based solutions meet the same industrial requirements.

A textured vegetable protein can be particularly interesting when manufacturers need an ingredient that can be stored, transported and dosed before being incorporated into a formulation. Compared with pre-hydrated plant-based matrices or finished products, the dry format offers greater flexibility in deciding when and how the ingredient is added to the recipe.

It also allows both the raw material and physical format to be tailored to the final product. A fine granule may integrate easily into certain mixes or fillings, while a larger piece may be preferred when a more defined presence is required within the finished preparation.

In industrial applications, this has a practical implication: the choice of texturate should be based on the final product and manufacturing process, not solely on the ingredient itself.

Technological functions in finished products

Texturates can fulfil a variety of functions within a formulation:

  • Providing bite and structure to plant-based products.
  • Integrating into blends for burgers, nuggets and fillings.
  • Contributing to texture in sauces and ready meals.
  • Absorbing water and flavours during hydration.
  • Maintaining appropriate structure throughout subsequent cooking or reheating processes, depending on the formulation.

This is why two products made with the same protein source can deliver very different results. The format, degree of texturisation and method of incorporation all have a direct impact on the final outcome.

Main formats and raw materials used in dry plant-based texturates

The raw material determines much of a texturate’s behaviour, but so does its physical structure.

When developing an industrial solution, both variables should be considered together: which ingredient is used and what texture is required.

At Sanygran, we primarily work with texturates made from soya, pea and blended plant-based ingredients, such as Legumeat®, a combination of soya flour, bean flour and rice flour.

The most common plant proteins in dry texturates

Soya remains one of the most widely used raw materials in plant-based texturates and enables the development of solutions suitable for a wide range of applications.

Pea protein has become one of the fastest-growing raw materials within the plant-based sector. In addition to offering strong technological performance, it allows manufacturers to develop formulations that avoid some of the industry’s most common allergens, such as soya and gluten.

There are also solutions based on blends of plant-based raw materials. This is the case with Legumeat®, Sanygran’s proprietary development, which combines soya flour, bean flour and rice flour to create a plant-based matrix that differs from texturates made from a single protein source.

The choice should not be based solely on the origin of the protein. It is equally important to consider texture, flavour, colour, hydration behaviour and end-use application.

Granulated, chunk and flake formats

The physical format influences how a texturate is incorporated into a recipe.

At Sanygran, we offer soya and pea texturates in fine granulated formats, particularly suited to formulations requiring homogeneous integration.

In the case of Legumeat®, in addition to fine granules, we also offer larger formats such as chunks and fillets for applications where a more defined plant-based structure is required.

Format selection depends on factors including:

  • The type of final product.
  • The desired level of integration.
  • The target texture.
  • The hydration process.
  • The mixing system.
  • The intended cooking or reheating method.

As a result, the same concept of a dry texturate can lead to very different solutions depending on the application.

How are dry plant-based texturates manufactured?

The production of a textured vegetable protein begins long before the ingredient reaches the customer’s production line.

Extrusion transforms plant-based raw materials into structures with specific physical characteristics. During the process, operating conditions within the extruder influence how this structure develops and, consequently, how the product performs afterwards.

The objective is not simply to create a plant protein with a specific shape, but to obtain a texturate that is stable, reproducible and suitable for subsequent hydration and industrial use.

Extrusion, drying and product stabilisation

Extrusion combines different processing conditions to transform raw materials and develop the texturate’s structure.

The product is then dried to achieve the conditions required for storage and handling.

This stage is particularly important because the end result must be consistent not only visually but also in its subsequent performance. When a customer incorporates a texturate into an industrial formulation, they need the ingredient to respond predictably from batch to batch.

In other words, the quality of a textured vegetable protein is measured not only when it leaves the extruder, but also by how it performs once rehydrated and incorporated into a formulation.

Process variables affecting texture and performance

Final texture depends on several extrusion process variables and the characteristics of the raw material itself.

These include factors such as:

  • Temperature, which influences raw material transformation.
  • Moisture, which affects structure development during extrusion.
  • Pressure and extrusion conditions, which determine the texture achieved.
  • Product size and shape, partly defined by the die system.
  • Final drying level, which is essential for product stability.

There is no universal combination that works for all applications. A texturate intended for a Bolognese sauce will not necessarily require the same characteristics as one designed for larger meat-free pieces.
For this reason, process control is just as important as raw material selection.

Criteria for selecting a dry texturate for plant-based applications

Selecting a texturate should not be reduced to comparing ingredients or prices per kilogram.

For R&D and purchasing teams, it is far more relevant to evaluate the performance the ingredient delivers within the intended application.

A texturate may be technically sound yet still not represent the best solution if it fails to suit the process, format or sensory objectives of the final product.

Compatibility with ready meals, fillings and meat alternatives

Dry texturates can be incorporated into a wide range of applications.

In burgers and nuggets, they can help create an integrated structure within the product matrix.

In fillings and Bolognese sauces, a granulated format can provide structure and recognisable texture without dominating the overall recipe.

In ready meals, selection must also take into account what happens after production, including cooking, reheating, storage and consumption.

For this reason, Sanygran works with different formats and raw materials suited to applications ranging from formed products to more complex prepared foods.

Selection factors: hydration, flavour, texture and cost

One advantage of dry texturates is that they can be designed around their behaviour during hydration.

At Sanygran, our texturates are manufactured in a neutral format, enabling them to absorb the flavour profile required by each formulation.

This is particularly valuable for manufacturers developing products with different sensory profiles. The same structural base can be used across multiple recipes with different seasonings, sauces and flavour directions without the ingredient competing with them.

When selecting a solution, it is also important to consider:

  • Hydration capacity and yield within the recipe.
  • Texture and bite after hydration.
  • Neutral flavour and aroma profile.
  • Batch-to-batch consistency.
  • Format and dosing convenience.
  • Actual application cost, rather than ingredient price alone.

This final point is especially important. The cost per kilogram of a texturate does not tell the whole story. It is essential to evaluate the value it adds to the formulation and the yield it delivers in the finished product.

Industrial advantages of dry plant-based texturates

The benefits of a dry format extend beyond formulation itself.

For food manufacturers operating at industrial scale, factors such as storage, transport, dosing and ingredient stability prior to use are equally important.

Shelf life, storage and logistics

As dry ingredients, texturates can be stored without the refrigeration requirements associated with pre-hydrated plant-based matrices, provided the recommended storage conditions are respected.

This can simplify logistics and allow manufacturers to stock ingredients before production begins.

In addition, the dry format can simplify handling and dosing operations, particularly in formulations requiring multiple ingredients to be added in controlled quantities.

Scalability and production repeatability

Moving from laboratory trials to industrial-scale production involves much more than simply increasing quantities.

Formulations must remain stable at larger scale, and ingredients must perform consistently across different batches.

In this context, a standardised textured vegetable protein supports accurate dosing, formulation control and process repeatability.

For manufacturers, this results in greater predictability when producing the same product repeatedly over time.

Food safety and quality control considerations for dry plant-based texturates

When an ingredient is destined for industrial food production, functionality is only one part of the equation.

Specifications, traceability, stability and storage conditions must also be controlled to ensure compliance with the requirements of the intended application.

Technical specifications and control parameters

Relevant texturate specifications may include:

  • Moisture content.
  • Particle size and format dimensions.
  • Batch uniformity.
  • Hydration performance.
  • Sensory characteristics.
  • Storage stability.

These parameters are not valuable in isolation. What matters is that they provide an ingredient that is predictable and compatible with the customer’s formulation and process.

For R&D teams, this predictability is essential when moving from initial trials to regular production.

Critical points in storage and handling

Although the dry format simplifies certain operations, the ingredient must still be protected from conditions that may compromise its stability.

Environmental moisture, cross-contamination, storage conditions and proper handling are all factors that must be considered during industrial use.

Furthermore, once hydrated, the texturate behaves very differently and becomes part of a matrix with its own storage requirements. For this reason, usage conditions should take into account both the dry ingredient and the finished product.

How can dry texturates be integrated into an industrial plant-based formulation?

Incorporating a dry texturate involves much more than simply adding it to a recipe.

Hydration, mixing and subsequent processing all influence the final outcome. Before scaling up a formulation, it is advisable to validate ingredient performance under real manufacturing conditions.

The relationship between hydration and final yield

When a texturate absorbs water, it increases in both weight and volume while developing the texture characteristics required in the formulation.

The amount of water used and the method of incorporation should be standardised to avoid production variability.

This has a direct impact on yield, as even small differences in hydration can affect texture, mixture consistency and subsequent product performance.

For this reason, industrial development requires more than simply knowing that a texturate “absorbs water”. Manufacturers need to understand how it performs within a specific formulation and under actual processing conditions.

Process adjustments during cooking, mixing and reheating

Every application has its own requirements.

A burger, a Bolognese sauce and a filling do not behave in the same way during mixing and cooking. Nor will they necessarily require the same conditions if the product is reheated later.

Before scaling up a formulation, it is therefore advisable to validate:

  • Texturate hydration.
  • Integration within the mix.
  • Texture after processing.
  • Behaviour during cooking.
  • Stability during reheating, where applicable.

The objective is to reach production with a formulation that not only works in the laboratory but is also fully reproducible in industrial manufacturing.

What can Sanygran offer as an industrial supplier?

Choosing a dry texturate is ultimately about choosing how a key part of the formulation will perform.

Having access to different raw materials, formats and adaptation possibilities allows product development to begin with the final application in mind rather than a standard ingredient.

At Sanygran, we work with soya, pea and blended plant-based ingredients such as Legumeat®, developing texturates for applications including burgers, nuggets, fillings, Bolognese sauces and ready meals.

Tailored development according to application and sales channel

Not all applications require the same size, texture or raw material.

For this reason, we can tailor different texturisation variables, including size, texture, ingredient and flavour.

All our texturates are manufactured with a neutral profile, making it easier to incorporate the desired flavour profile during hydration. This allows products with distinct sensory characteristics to be developed from the same technological base, adapting to each recipe and brand positioning strategy.

Technical support from formulation to industrialisation

The value of a texturate supplier extends beyond simply supplying an ingredient. To achieve successful industrial performance, it is essential to understand how the ingredient integrates, hydrates, processes and contributes to the final product.

At Sanygran, we support development from raw material selection and identification of the most suitable solution through to formulation trials and adaptation to production requirements.

In this way, texturates become more than just raw materials. They become a development tool that delivers structure, texture and functionality from the earliest stages of a project.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

High-Moisture Plant-Based Texturates

High-Moisture Plant-Based Texturates

  • High-moisture plant-based texturates make it possible to create fibrous, juicy, and stable structures, closer to a meat-like experience than traditional TVP.
  • They add value in prepared meals, fillings, foodservice, retail, and private label, maintaining integrity during cooking, regeneration, chilling, and freezing.
  • Selection must be validated according to texture, shelf life, and the customer’s process: moisture, formulation, storage, cooking, syneresis, and batch-to-batch scale-up are critical.

Achieving a convincing plant-based texture is no longer solely a matter of formulation. High-moisture plant-based texturates have become one of the most promising technologies for developing plant-based alternatives with a fibrous structure, juicy bite and stable performance throughout the manufacturing process.

Thanks to high-moisture extrusion, it is now possible to create products capable of replicating the eating experience of meat while adapting to applications as diverse as ready meals, foodservice solutions, and products intended for retail and private label markets.

In this article, you will discover what high-moisture texturates are, how they are manufactured, the benefits they bring to the food industry, and why more and more manufacturers are incorporating them into new product developments.

What Are High-Moisture Plant-Based Texturates?

High-moisture plant-based texturates are products made from plant proteins that, through a high-moisture extrusion process, develop a fibrous structure very similar to that of meat.

Put simply, these are plant proteins that move beyond the form of powders or granules and become structured pieces with a defined texture, a juicy bite and suitability for a wide range of food applications.

The main difference compared with a traditional textured vegetable protein (TVP) is that the product leaves the process with a high moisture content, making it possible to achieve a more fibrous texture, a more realistic bite and greater juiciness.

For food manufacturers, this represents a significant advantage, as it facilitates the development of plant-based products ready to be incorporated into recipes, reducing processing stages and improving consistency in the final result.

In addition, these texturates can be used in both chilled and frozen products, adapting to different preservation, distribution and shelf-life requirements.

Industrial Applications of High-Moisture Texturates

The principal advantage of this technology is its versatility.

Depending on the formulation, cut and flavour profile, the same process can deliver completely different applications.

Chilled and Frozen Ready Meals

Ready meals are one of the categories where these products provide the greatest value.

Their structure remains intact throughout cooking, regeneration, chilling and freezing processes, enabling manufacturers to develop recipes that remain consistent right up to the point of consumption.

For this reason, they are particularly attractive for producers of ready meals, premium convenience foods and ready-to-eat solutions.

Fillings, Sauces and Mixed Preparations

They also perform exceptionally well in applications where they are combined with other ingredients.

Plant-based Bolognese sauces, pasta fillings, pizzas, wraps, tacos, prepared rice dishes and sauces are just some examples where texturates provide structure while maintaining stability throughout the product’s shelf life.

Their ability to absorb flavours makes them easy to incorporate into complex recipes while retaining a distinct texture.

Products for Retail and Private Label

In products intended for large-scale retail distribution, consistency is just as important as the recipe itself.

High-moisture texturates make it possible to achieve uniform products from batch to batch, with excellent appearance and stable performance during chilled or frozen storage.

This facilitates the launch of new retail and private-label products, where product consistency is a key requirement.

How Are High-Moisture Texturates Produced and Processed Industrially?

Final product quality does not depend solely on machinery.

The selection of raw materials, formulation design and control of the entire production process determine the texture, juiciness and subsequent performance of the product.

Raw Materials and Formulation

The plant proteins selected play a major role in determining the final result.

At Sanygran, we primarily work with soy and pea proteins, two raw materials that offer excellent functional properties for these applications.

In addition, our R&D team has developed projects using ingredients such as brewers’ spent grain, which contributes to circular economy initiatives and has been used in products such as our plant-based beef alternative, as well as oats, which provide a softer bite and a particularly pleasant texture.

Each raw material behaves differently during extrusion, making the right combination essential to achieving the desired product performance.

Texturisation and Moisture Control

During extrusion, controlling moisture is one of the most critical aspects of the process.

Variables such as water content, temperature and processing speed directly influence the formation of plant-based fibres.

Precise control allows manufacturers to obtain highly juicy products with a uniform texture and excellent storage stability.

By adjusting these parameters, it is also possible to develop products with either a denser or a lighter structure, depending on the requirements of the final application.

Cooling and Conditioning

Once the desired structure has been achieved, an equally important phase begins.

Cooling helps to stabilise the internal structure and preserve the texture obtained during extrusion.

The product is then conditioned according to the target application and required final format.

At Sanygran, we commonly work with formats such as chunks, pulled-style strands and flakes, among others.

This variety enables each customer to find the most suitable solution for their recipe without modifying their manufacturing process.

Functional Benefits of High-Moisture Plant-Based Texturates for Food Manufacturers

High-moisture texturates do more than replace animal-derived ingredients. They can also help optimise processes, improve product stability and reduce development times.

Texture and Eating Experience

One of the main challenges in any meat analogue is delivering a convincing eating experience.

Thanks to high-moisture extrusion, it is possible to achieve different levels of fibrousness, juiciness, firmness and bite, tailoring the product to the outcome each customer is seeking.

Developing strips for fajitas requires a different texture from that needed for a plant-based lasagne filling or chunks designed to accompany a rice dish. Each application demands a specific texture and therefore a dedicated manufacturing approach.

In addition to texture, the sensory profile can also be customised. At Sanygran, we develop different flavour profiles, including chicken, beef and seafood-inspired concepts such as plant-based tuna or salmon, enabling each development to align with the brand’s positioning.

Formulation Efficiency and Manufacturing Performance

One of the less visible but most important advantages for manufacturers is process efficiency.

As ready-to-use ingredients, these products can simplify certain production stages and contribute to greater consistency between batches.

This translates into:

  • More efficient processes.
  • Reduced preparation time.
  • Greater manufacturing repeatability.
  • Improved utilisation of raw materials.

For manufacturers producing high volumes, these improvements can have a direct impact on productivity and product consistency.

Versatility Across Recipes and Formats

A single technology can be used to develop a wide variety of solutions.

Depending on the application, texturates can be used:

  • As a plant-based alternative to meat or fish, ready for incorporation into recipes.
  • As a base ingredient for developing higher-value plant-based products such as burgers, nuggets, meatballs and various finger food concepts.

This versatility enables manufacturers to address different market needs and develop multiple applications from a single technology platform.

Technical Criteria for Selecting a High-Moisture Texturate

Not every project requires the same type of texturate.

Before selecting a solution, it is important to analyse how the product will perform throughout its entire lifecycle.

Texture Profile and Cooking Performance

Initial texture is important, but maintaining it after cooking is even more critical.

For this reason, product performance should be validated during processes such as:

  • Cooking
  • Regeneration
  • Reheating
  • Freezing and thawing

The objective is to ensure that the texture remains stable from production through to the moment of consumption.

Shelf Life, Preservation and Microbiological Stability

When working with high-moisture products, preservation becomes a critical factor.

Formulation, packaging systems and storage conditions all directly influence shelf life.

For this reason, each development should be validated under real manufacturing and distribution conditions to ensure stability throughout the commercial lifecycle.

Compatibility with the Customer’s Production Process

Developing a good product is only part of the challenge. It must also integrate easily into the customer’s manufacturing process.

Factors such as mixing, dosing, filling and packaging can influence overall performance.

For this reason, during development it is important to adapt the behaviour of the texturate to the customer’s real manufacturing requirements and not solely to its organoleptic properties.

Challenges in Manufacturing High-Moisture Plant-Based Texturates and How to Overcome Them

High-moisture extrusion offers significant opportunities, but it also presents technical challenges that must be controlled from the outset.

Moisture Management and Syneresis Prevention

One of the main challenges is maintaining the correct balance between juiciness and stability.

Excess water or insufficient process control can lead to liquid release during storage or changes in texture.

This is why both formulation and extrusion parameters must be carefully optimised, alongside appropriate preservation conditions.

Batch Consistency and Industrial Scale-Up

Achieving good results at pilot scale is only the first step.

The real challenge lies in reproducing exactly the same texture when producing thousands of kilograms at industrial scale.

To achieve this, it is necessary to maintain strict control over raw materials, moisture, temperature and extrusion parameters, ensuring maximum batch-to-batch repeatability.

This consistency is particularly important for retail and private-label products, where consumers expect the same product every time they purchase it.

Tailoring Solutions to Each Project

Every customer has different requirements.

Some are looking for a highly fibrous texture for a chicken alternative, while others require a softer structure for ready meals or seafood-inspired solutions.

For this reason, at Sanygran, development begins by understanding the final application and adapting both the formulation and the process to achieve exactly the performance required for each project.

What Should a B2B Supplier of High-Moisture Plant-Based Texturates Offer?

Choosing a supplier is not simply a matter of comparing technical specifications.

It also means working with a team capable of supporting product development from the earliest trials through to full-scale production.

Joint Development and Specification Optimisation

Every project starts with different requirements.

That is why we work closely with customers to define aspects such as:

  • Texture
  • Format
  • Flavour profile
  • Shelf life
  • Preservation system

This collaborative approach helps reduce development times and minimise adjustments once production begins.

Technical Support During Industrial Implementation

Introducing a new ingredient into a manufacturing process requires validation and adjustments to ensure optimal performance at industrial scale.

During this phase, factors such as texture, moisture, dosing and integration into the production line may need to be addressed.

Having specialised technical support facilitates implementation, reduces adaptation time and helps minimise risks before commercial launch.

A Partner for Developing High-Moisture Plant-Based Solutions

At Sanygran, we develop and manufacture high-moisture plant-based texturates tailored to the requirements of each project.

We collaborate with food manufacturers, private-label brands and the wider food industry to create customised solutions in terms of format, texture and sensory profile.

We support our customers from product development through to industrial implementation, helping bring new products to market efficiently and successfully.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

Traceability in Plant-Based Products

Traceability in Plant-Based Products

  • Traceability in plant-based products makes it possible to control raw materials, processes, and finished products, from ingredient receipt through to final customer delivery.
  • A robust system requires recording batches, formulations, production orders, quality controls, and dispatches, making audits, complaints, and incident management easier.
  • Traceability impacts safety, quality, and scalability: it helps manage allergens, recalls, batch-to-batch consistency, shelf life, and industrial growth without losing control.

In this article, we explore traceability in plant-based products, a key element in ensuring control over raw materials, manufacturing processes and finished products throughout the production of plant-based foods.

Traceability enables manufacturers to track the complete journey of a product, from ingredient intake to delivery to the end customer. In the plant-based sector, where multiple raw materials, suppliers and formulation variations are involved, having a robust traceability system simplifies quality control, improves responsiveness to issues and provides greater security throughout the production process.

Furthermore, for manufacturers supplying retailers, private label brands and foodservice operators, traceability has become an essential requirement for guaranteeing supply reliability, meeting quality standards and responding quickly to audits or incidents.

What Does Traceability Require in the Plant-Based Supply Chain?

Traceability requires manufacturers to identify which raw materials are included in each batch, how they have been used during production and to which customers the final products have been supplied.

To achieve this, it is necessary to maintain organised records covering ingredients, batches, manufacturing processes, formulations and product dispatches. It is not simply about regulatory compliance; it is about having reliable information available to make rapid decisions when issues or customer complaints arise. Well-managed traceability also supports continuous improvement, enabling manufacturers to identify deviations, analyse trends and optimise both production processes and product quality.

Critical Traceability Points for Ingredients and Finished Products

Traceability must be maintained from the receipt of raw materials right through to finished product dispatch. The most sensitive stages are typically:

  • Ingredient intake
  • Formulation
  • Manufacturing
  • Packaging
  • Storage
  • Distribution

Any loss of information at these stages can make it difficult to reconstruct the complete history of a production batch. Information commonly recorded includes:

  • Raw material batch numbers
  • Production orders
  • Quality control checks
  • Production dates
  • Finished product destinations

This makes it possible to rapidly reconstruct the complete journey of any product reference whenever required.

Internal Traceability vs Customer Traceability

Internal traceability allows manufacturers to monitor the movement of raw materials within the production facility and understand how they are transformed into finished products.

Customer traceability, on the other hand, identifies which batches have been supplied to each manufacturer, distributor or retail chain.

These two levels are complementary. While internal traceability supports production process control, customer traceability enables the rapid localisation of specific batches in the event of an issue, minimising the impact on wider production.

How Is Traceability Applied in Plant-Based Manufacturing?

Traceability should be embedded within day-to-day operations and maintained throughout every stage of production.

In plant-based food manufacturing, where it is common to work with different plant proteins, fibres, starches, functional ingredients and frequent formulation adjustments, precise monitoring is essential to ensure product consistency and repeatability.

Raw Material Intake and Supplier Control

Every traceability process begins with ingredient receipt. Each raw material should be correctly identified and linked to the relevant documentation, including:

  • Supplier details
  • Original batch number
  • Date of receipt
  • Technical specifications
  • Applicable certificates

Whenever a new supplier is introduced or a specification changes, the raw material must also be validated and documentation updated to maintain the integrity of the traceability system.

Monitoring During Formulation and Production

Traceability does not end once ingredients enter the factory. Throughout production it is equally important to record information relating to:

  • Recipes used
  • Formulation versions
  • Manufacturing orders
  • Process parameters
  • Quality control activities

In plant-based products, even minor adjustments can influence texture, stability or industrial performance. Maintaining a detailed production history makes it easier to investigate deviations and consistently reproduce manufacturing conditions.

Batch Identification During Packaging and Dispatch

The final stage involves correctly identifying the finished product. Effective coding systems enable every unit to be linked to:

  • Raw materials used
  • Manufacturing date
  • Production line
  • Packaging format
  • Destination customer

This information is essential for warehouse management, logistics efficiency and rapid intervention whenever a specific batch must be blocked, isolated or recalled.

Traceability, Food Safety and Risk Management

Traceability is directly linked to food safety and a company’s ability to manage risk effectively.

A comprehensive traceability system has limited value if information cannot be retrieved quickly when an issue occurs. The ability to rapidly identify a batch, determine which raw materials were used and establish which customers received the product can make the difference between a minor corrective action and a major operational problem.

Allergen Control and Cross-Contamination Prevention

Many plant-based products contain potentially allergenic ingredients such as soya or gluten. For this reason, it is essential to maintain records relating to:

  • Batches used
  • Production sequences
  • Cleaning procedures
  • Verification activities

These controls help prevent cross-contamination, support internal investigations and strengthen audit readiness.

Product Recall and Reverse Traceability

Reverse traceability enables manufacturers to determine precisely which raw materials were used in any particular batch and where that product has been distributed. This makes it possible to identify:

  • Affected product references
  • Customers who received the products
    Products requiring withdrawal or market recal

The faster and more accurately this process can be completed, the lower the financial, operational and commercial impact on the manufacturer.

Traceability Requirements by Sales Channel

Not all customers require the same level of information. Traceability in plant-based products must be adapted to the sales channel, product category and documentation requirements of each project.

Requirements for Prepared Meal Manufacturers

Companies incorporating plant-based ingredients or products into their own recipes require reliable information regarding:

  • Batch identification
  • Product specifications
  • Shelf life
  • Product stability
  • Processing performance

A well-structured traceability system simplifies ingredient integration, reduces uncertainties during product development and provides greater confidence when formulations are modified or scaled up.

Expectations of Food Manufacturers and Distributors

Manufacturers and distributors often require a high degree of documentation and process control to guarantee supply continuity.
In addition to technical specifications, they frequently request information on:

  • Batch history
  • Formulation changes
  • Certifications
  • Audit results
  • Incident management procedures

Having this information available and organised strengthens supplier-customer relationships and supports successful audits and supplier approvals.

Traceability for Retail and Private Label Products

Projects supplying retailers and private label brands generally require particularly robust traceability systems.

Accurate batch identification, shelf-life control, supporting documentation and the ability to quickly locate individual product references provide reassurance for both manufacturers and distribution partners. In these projects, traceability forms a fundamental requirement for maintaining a stable and consistent supply.

Technologies and Systems That Improve Traceability in the Plant-Based Industry

Digitalisation has transformed traceability management in plant-based food manufacturing.

Today, many businesses operate with integrated ERP systems, data capture solutions and document control platforms that enable real-time information recording while reducing errors associated with manual processes.

The goal extends beyond storing information; it is ensuring that information can be recovered quickly whenever it is needed.

Coding, Labelling and Data Capture

Correct identification through batch coding and labelling systems enables products to be tracked from raw material intake through to dispatch. This helps organisations to:

  • Quickly identify any batch
  • Accelerate audits
  • Reduce identification errors
  • Improve logistics management

A clear coding system also simplifies communication between production, quality, warehouse and customer teams.

Digital Records and Document Control

Digital management systems make it possible to centralise all manufacturing-related information. This allows rapid access to:

  • Formulation changes
  • Supplier history
  • Technical specifications
  • Production records
  • Quality control documentation

A complete traceability system is only effective if information can be retrieved quickly when incidents occur. Accessible records improve decision-making and reduce response times when problems arise.

How Does Traceability Impact Product Quality, Shelf Life and Scalability?

Traceability is not simply a documentation requirement. It also contributes directly to product quality, process repeatability and industrial scalability.

When information is correctly recorded throughout production, manufacturers can more easily identify deviations, implement corrective actions and maintain product consistency.

Organoleptic Consistency Between Batches

Accurate recording of ingredients, formulation versions and manufacturing conditions helps maintain greater consistency in:

  • Texture
  • Flavour
  • Appearance
  • Cooking performance

If a deviation occurs, traceability enables its origin to be identified quickly and corrective measures implemented before future production runs are affected.

Shelf Life and Supply Chain Stability

The stability of a plant-based product depends on numerous factors that must remain under control throughout the supply chain.

Traceability links each production batch to manufacturing, storage and transport conditions, supporting the investigation of issues related to shelf life, cold chain integrity and product performance during distribution.

Industrial Scale-Up Without Losing Batch Control

As production volumes increase, process complexity grows accordingly.

A robust traceability system enables manufacturers to manage multiple product references, suppliers and production orders without losing visibility over individual batches.

This supports industrial growth while maintaining repeatability, quality control and supply reliability. In addition, historical records provide valuable information for continuous improvement, trend analysis and long-term manufacturing process optimisation.

What Should an Industrial Customer Expect from a Plant Based Supplier Regarding Traceability?

When selecting a plant-based manufacturing partner, traceability should be considered a key evaluation criterion from the outset.

It is not simply about receiving documentation; it is about working with a supplier capable of providing reliable information, responding rapidly to incidents and maintaining product consistency between batches.

Technical Documentation and Product Specifications

Among the most valuable documents are:

  • Up-to-date technical data sheets
  • Batch identification records
  • Storage conditions
  • Shelf-life information
  • Product specifications
  • Audit and traceability documentation

At Sanygran, we develop plant-based food manufacturing projects supported by traceability systems that allow complete product monitoring, from raw material intake through to final dispatch.

Working with a partner that integrates traceability throughout the entire manufacturing process enables companies to respond efficiently to audits, maintain documentary control and provide greater assurance when products are destined for retail, private label or highly demanding distribution channels.

Because effective traceability is not simply about recording information — it is about having access to that information when it truly matters, enabling informed decisions, rapid issue resolution and uninterrupted supply continuity.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com

Chilled Plant-Based Product Supplier

Chilled Plant-Based Product Supplier

  • A chilled plant-based product supplier must guarantee shelf life, stability, food safety, and reliable supply, not just manufacture an appealing recipe.
  • The formulation must be validated according to application and storage conditions: texture, flavor, bite, cohesion, microbiological stability, packaging, cold chain, and industrial compatibility.
  • Supplier selection requires flexibility and technical support: custom development, batch-to-batch consistency, traceability, supply continuity, and scale-up capability.

When a company searches for a chilled plant-based product supplier, it needs far more than a manufacturer capable of producing a recipe. Shelf life, product stability, food safety, supply reliability and compatibility with industrial processes are all decisive factors in determining whether a product can succeed in the marketplace.

In chilled categories, where the cold chain, logistics and storage times require greater control than dry or frozen products, choosing the right supplier can make the difference between a successful launch and a product that struggles to gain traction.

For this reason, manufacturers and distributors evaluate not only the finished product, but also the technical expertise, industrial experience and quality systems that support every development.

What Should You Expect from a Chilled Plant-Based Product Supplier?

A chilled plant-based product supplier should be able to ensure that a product maintains its characteristics from manufacture through to consumption or integration into another industrial process.

Achieving this requires a combination of production capacity, quality control, cold chain management and the flexibility to adapt to different technical and commercial requirements.

Capacity to Manufacture at Industrial Scale

Scalability is one of the most important considerations when developing chilled products.

A formulation that performs well at laboratory scale must be capable of being reproduced consistently at industrial scale, maintaining uniform quality between batches and ensuring continuity of supply.

It is equally important that the supplier can respond to increased production volumes, new product references or fluctuations in demand without compromising product stability, food safety or delivery schedules.

Quality Control and Food Safety

Chilled plant-based products require continuous monitoring of raw materials, production processes and storage conditions.

Factors such as traceability, microbiological control, shelf-life validation and strict hygiene procedures are essential to guarantee both product safety and stability throughout its intended lifespan.

For businesses supplying retailers or private-label brands, robust quality systems also support audits, approvals and compliance with the documentation requirements demanded by major retail chains.

Adapting to the Needs of Industrial Customers

Every project has different requirements.

Some manufacturers are looking for a plant-based ingredient to incorporate into their own formulation, while others need a finished product ready for sale under their own brand.

A reliable supplier should therefore be capable of adapting the formulation, texture, format, packaging type, shelf life and product performance according to the distribution channel, production process and customer objectives.

Types of Chilled Plant-Based Products for the Food Industry

Chilled plant-based products cover a wide range of categories, each with specific formulation, preservation and industrial application requirements.

Chilled Plant-Based Ingredients

Chilled ingredients allow manufacturers to incorporate plant protein and technological functionality into other formulations.

These solutions are commonly used in ready meals, chilled recipes and new product developments, where plant-based ingredients must be integrated without compromising stability throughout the cold chain.

Their main advantage is that they simplify the incorporation of plant-based ingredients while maintaining consistent performance during both processing and storage.

Finished Chilled Plant-Based Products

This category includes products such as plant-based burgers, plant-based nuggets, chicken-style pieces, tofu, hummus, seitan and falafel.

These products can be supplied as finished goods, ready for commercialisation or integration into professional foodservice channels and private-label projects.

For these applications, factors such as shelf life, microbiological stability, sensory profile and ease of handling are critical to maintaining consistent performance throughout the supply chain.

Technical Factors That Influence Chilled Plant-Based Product Formulation

The success of a chilled plant-based product depends on achieving the right balance between formulation, industrial processing and preservation. Ingredient selection is important, but understanding how ingredients interact and behave throughout manufacturing and shelf life is equally essential.

Texture, Flavour and Application Performance

Formulations should be designed according to the intended end use.

In products aiming to deliver a meat-like experience, attributes such as bite, cohesion, juiciness and sensory profile are particularly important.

It is also advisable to evaluate from the early development stages how the product performs during cooking, reheating, pasteurisation or incorporation into larger recipes, helping to avoid issues when moving to industrial-scale production.

Chilled Stability and Shelf Life

Shelf life remains one of the greatest challenges in chilled products.

Maintaining microbiological stability while preserving sensory quality requires careful control of formulation, storage conditions, the cold chain and the packaging system.

For this reason, shelf-life validation should form part of the development process from the outset rather than being addressed at the end.

Technologies such as Modified Atmosphere Packaging (MAP) and post-pack pasteurisation can help extend shelf life, although the most appropriate solution depends on the product type, formulation and commercial objectives.

Compatibility with Industrial Processes

Products must also integrate efficiently into the customer’s production environment.

Factors such as mechanical resistance, ease of handling, cooking performance and compatibility with different production lines are essential for efficient manufacturing and for minimising issues during industrial scale-up.

How Chilled Plant-Based Products Fit into Production and Distribution Chains

Managing chilled plant-based products requires control at every stage, from manufacturing through to delivery. Maintaining the cold chain, ensuring traceability and protecting product quality are all crucial to ensuring products reach the market in optimal condition.

Packaging and Chilled Preservation

Packaging plays a critical role in protecting products throughout their shelf life.

In addition to simplifying storage and distribution, it must help preserve quality, minimise the risk of external contamination and maintain the required preservation conditions for each reference.

The choice of packaging system will depend on the product type, sales channel, logistics requirements and target shelf life.

Distribution and Cold Chain Maintenance

One of the greatest challenges associated with chilled products is maintaining an uninterrupted cold chain during storage, transportation and distribution.

Any deviation may affect food safety, microbiological stability, texture and actual shelf life.

For this reason, effective temperature control must be combined with comprehensive traceability systems that allow each batch to be tracked and facilitate rapid action in the event of any incident.

What Does a Specialist Chilled Plant-Based Supplier Offer Ready Meal Manufacturers and Food Producers?

Working with a specialist supplier does more than simplify production. It can also reduce development times, minimise technical challenges and accelerate the industrialisation of new products.

Support During Product Development

Many projects do not start from scratch. In some cases, the objective is to optimise an existing recipe, replicate a product already on the market or adapt it to new commercial requirements.

In these situations, collaboration between manufacturer and customer helps to adjust formulations, validate industrial performance and confirm that the product maintains its specifications before large-scale production begins.

Process Optimisation and Reduced Production Issues

A well-developed formulation can help minimise problems related to texture, exudation, stability and processing performance.

This contributes to reducing waste, rework and batch variations, leading to more efficient production and improved product consistency.

Adaptation to Sales Channels and End Use

Each channel presents its own technical requirements.

A product designed for retail distribution requires different characteristics from one intended for foodservice or from an ingredient destined for incorporation into a ready meal.

Consequently, elements such as format, preservation system, presentation and shelf life should be defined from the earliest stages of development to ensure the product meets the practical requirements of its intended application.

Criteria for Choosing a Chilled Plant-Based Product Supplier

Selecting a chilled plant-based product supplier involves evaluating much more than the finished product itself. The ability to support development, guarantee quality and ensure supply continuity is equally important.

Flexible Formulation and Custom Product Development

Each project has unique requirements regarding texture, sensory profile, shelf life and industrial performance.

Working with a supplier capable of developing bespoke formulations, conducting trials and validating modifications before industrialisation can significantly reduce development cycles and speed up market launch.

Consistency, Traceability and Technical Support

Batch consistency, traceability and technical support are essential to ensuring dependable supply.

In addition to facilitating issue resolution, they support formulation adaptation, process changes and compliance with audits and documentation requirements—particularly within private-label and large-scale retail projects.

Industrial Viability and Continuity of Supply

Suppliers must be capable of maintaining stable production and responding effectively to customer growth requirements.

Ensuring continuity of supply, batch repeatability and the ability to adapt to increased production volumes is essential when a product forms part of an established manufacturing process or commercial range.

Sanygran as a Supplier of Chilled Plant-Based Solutions for the Food Industry

At Sanygran, we develop and manufacture chilled plant-based foods for manufacturers, ready meal producers, distributors and private-label projects.

Our portfolio includes products such as plant-based burgers, nuggets, chicken-style pieces, tofu, hummus, seitan and falafel, alongside customised developments tailored to individual customer requirements.

Our experience as both ingredient manufacturers and finished product producers allows us to understand how formulation, processing and preservation influence final product performance. This helps validate solutions under real manufacturing conditions and identify potential improvements before industrial scale-up.

We also offer technologies such as Modified Atmosphere Packaging (MAP) and post-pack pasteurisation, enabling the most appropriate preservation strategy to be selected according to the product, target shelf life and logistical requirements.

For companies seeking a specialist industrial partner in plant-based food manufacturing, working with a supplier involved from formulation development through to production and long-term supply can help reduce development times, minimise industrialisation issues and bring more stable and competitive products to market.

Contact:

📞 +34 937 132 324
✉️ info@sanygran.com